Hey everyone! If you’ve ever worked in mining, quarrying, agriculture, logistics, or any industry that moves bulk materials day in and day out, you’ve probably seen a sidewall conveyor belt in action. They’re those bad boys that don’t just carry stuff along a flat line—they lift and tilt too, turning flat conveyor routes into sloped or even vertical paths that would make standard belts slip, spill, or stall. As someone who’s been in the sidewall conveyor belt game for years (I actually run a small, hardworking team supplying these exact belts to companies across North America), I get so many questions from customers and even fellow industry folks: “What are these things made of, anyway?” It’s not just the same old rubber you see on a regular flat belt, right? So let’s break this down like we’re chatting over a coffee, no stuffy textbook jargon, just real, usable info that actually matters if you’re buying, using, or just curious. Sidewall Conveyor Belt

First off, let’s get the basics straight for anyone new here. A sidewall conveyor belt isn’t one single material—it’s a layered Frankenstein (in the best way) of different components, each doing a specific job. Think of it like a sandwich: the bread is the core, the fillings add structure, and the toppings handle the messy stuff like spills, bumps, and grime. Wait, actually, it’s more like a custom power tool—every part is engineered for a exact task, and you can’t swap them willy-nilly or the whole thing breaks. That’s the key point I wish everyone knew: the material mix depends entirely on what you’re moving, how steep the slope is, how fast your line runs, and what kind of environment you’re working in. There’s no “one size fits all” here, which is why I always tell customers not to just order the cheapest belt off the shelf—it’ll cost you more in downtime later.
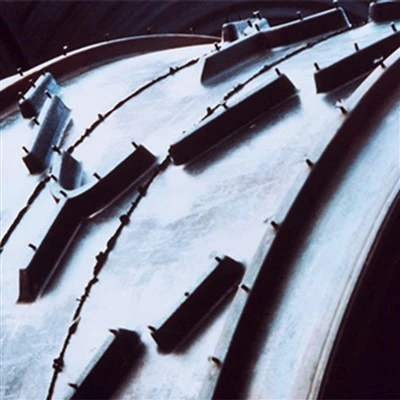
Let’s start with the absolute most important layer, the one that makes this a sidewall belt, not a regular one: the sidewalls themselves. These are those tall, rubbery (mostly) strips bolted to the edges of the core belt, right? Their whole job is to stop your material from sliding off as the belt climbs up a 30, 45, even 90-degree slope. If the sidewalls don’t hold, you’re spending half your shift picking up spilled gravel, grain, or whatever you’re moving instead of getting work done. So what are they made of?
Most standard sidewalls are natural rubber, but wait—natural is the base, they blend it with synthetic rubber for extra oomph. I’m talking styrene-butadiene rubber (SBR) is the go-to here, sometimes neoprene if you need it tougher. Why blend? Natural rubber is stretchy, good for flexing over pulleys, but it wears out fast if you’re moving sharp, abrasive stuff like rock or ore. SBR is tougher, more resistant to scrapes and tears, so mixing the two gives you that perfect balance: flexible enough to bend around rollers, but tough enough to take a beating. For industries that deal with super hot materials—like cement plants moving clinker that’s 200+ degrees Fahrenheit—we use heat-resistant sidewalls, usually with synthetic rubber blends that hold up without melting or breaking down. And if you’re in a place like the Gulf Coast where it’s super humid, or up north where it freezes solid in winter, we add anti-slip compounds to the sidewalls so they don’t get slick when it’s raining or ice forms. No one wants a belt that can’t grip when it’s time to work.
Then there’s the corrugated profile—the little vertical ridges between the sidewalls that actually cradle your material. These are super important because they fill the gap between the sidewalls and the core belt, creating a sort of trough that doesn’t let anything fall out. What are those ridges made of? Same rubber blend as the sidewalls, but usually a little softer? Wait no—actually, they’re a bit more flexible so they can compress a tiny bit when the belt turns around the end pulleys, without cracking. If the corrugations get stiff, they’ll split within a week. I’ve seen that happen before with cheap belts: the ridges pop right off, and suddenly you’ve got an open belt spilling all over the place. The good stuff has corrugations bonded permanently to the sidewalls, not just glued on, so they move as one piece. That’s a quality check I always tell customers to ask for when they’re comparing options.
Now, moving to the core of the belt—the part that runs along the pulleys, bears all the weight, and keeps everything from tearing through the middle. This is where most of the heavy lifting happens, and there’s way more variation here than people realize. The core material is what decides how much weight the belt can carry, how much stretch it has, and how long it lasts before the whole thing snaps. Let’s start with the old-school core: cotton canvas. Yeah, that’s right, back in the day most belts were made with layers of cotton fabric soaked in rubber. It works fine for light-duty stuff—like moving grain on a small farm, or low-volume logistics. But cotton stretches a lot, especially when it’s loaded up with heavy material. I’ve had a farmer come to me once complaining his old cotton-core belt was sagging so bad on a 20-degree slope that grain was sliding right off. Solution? Switched to a polyester blend core, and he hasn’t had an issue since.
Wait, polyester is the next big one. Polyester (PET, the same plastic in water bottles, fun fact) cores are way stronger than cotton, stretch way less, and hold up way longer. Most of our medium to heavy-duty sidewall belts use polyester core plies—usually 2 to 6 layers, depending on how heavy your load is. Each ply is a woven fabric that’s coated in rubber to keep it from fraying or absorbing moisture. The best part? Polyester doesn’t rot if it gets wet, which is a huge win for mines, quarries, or any outdoor operation that deals with rain or water runoff. I had a gravel company up in Ohio last year whose old cotton core belts would start falling apart within 6 months because they were exposed to constant mud and rain. Switched to polyester core, and those belts are still going strong 18 months later. No rot, no extra sag, way less downtime.
But wait, what about super heavy-duty stuff? Like mining, where you’re hauling tons of ore, or steel mills moving hot, sharp metal scraps? Then we go to the big boys: steel cord cores. These are not fabric—they’re thin, high-tensile steel wires twisted together, coated in rubber to stop corrosion. Steel cord is way stronger than any fabric core, stretches almost nothing, and can handle way higher loads. I’m talking belts that can carry 100+ tons per hour, climbing 50-degree slopes, no problem. The only downside? They’re more expensive, and if they get punctured by a sharp piece of metal, the steel can rust and spread, leading to a big tear. But for the right job, they’re worth every penny. Last year we supplied a copper mine in Arizona with steel cord sidewall belts, and they told us it cut their belt replacement time by 40% because they don’t have to swap out belts every 3 months like they did with fabric cores.
Then there’s the cover of the belt—the top and bottom layers that touch the material and the pulleys. This is what everyone sees on the flat part, but it’s just as important as the sidewalls. The top cover (the one carrying the material) is made of rubber blends tailored to what you’re moving. If you’re moving sharp, abrasive stuff like rock or ore, you need an abrasion-resistant cover—usually SBR blended with carbon black to make it tougher. That carbon black doesn’t just make it black (though it does, obviously), it resists scraping and wearing down from all that grit rubbing against it. If you’re moving sticky stuff like wet clay or fertilizer, you need a tear-resistant cover that also doesn’t let the material stick. We use a special blend of natural rubber and neoprene for that, which is smooth but grippy, so the clay slides off easily when you’re done. And if you’re moving food-grade materials—like grain, sugar, or flour—we have FDA-approved covers made with food-safe rubber that doesn’t leach chemicals, because you don’t want your flour tasting like old rubber, right? That’s a non-negotiable for food and beverage operations.
The bottom cover (the one that rides on the pulleys and rollers) is a bit different. It needs to be resistant to friction from the rollers, so it doesn’t wear out fast, and it has to grip the pulley properly so the belt doesn’t slip. Usually it’s a thicker, more durable rubber blend, often with anti-static properties if you’re working in an area where dust can build up and cause static sparks—like grain silos or coal mines. Static sparks are a fire hazard, so that anti-static cover is non-negotiable there. I learned that the hard way a few years back: a small local coal mine had a cheap belt without anti-static, and a static spark from the belt caused a dust explosion, shutting them down for a month. Switched to our anti-static sidewall belts, and they haven’t had an issue since.
Wait, I can’t forget about some of the specialized additives that go into these materials, because they’re the unsung heroes. Like, if you’re working in super cold climates (think places like Minnesota or Canada where winter temps drop below -20°F), we add plasticizers to the rubber so it doesn’t get brittle and crack. If you’re working in super hot climates (like Texas or the Middle East, where temps hit 120°F), we add heat stabilizers so the rubber doesn’t melt or break down from UV exposure—since a lot of these lines are outdoors, right? And for belts that need to flex a lot, like those that go around tight pulleys, we add flexibility agents so the sidewalls and corrugations don’t snap when the belt bends.
Let me be real here: a lot of cut-rate suppliers will cut corners on these materials to save a buck. They’ll use only natural rubber in the sidewalls, no blend with SBR, so it wears out in months. They’ll use thin cotton core instead of polyester, so it stretches and sag after a few weeks. They’ll use a cheap cover with almost no carbon black, so it tears if you look at it wrong. I’ve seen this happen so many times, and it’s a huge headache for the customer. They think they’re getting a deal, but really they’re spending more on emergency replacements, downtime, and labor than if they’d bought a quality belt from the start. That’s why I always tell customers to ask for the full material specs when they’re shopping. Don’t just take a supplier’s word that it’s “heavy-duty”—ask what the core is made of, what the sidewall rubber blend is, what the cover’s abrasion resistance is rated for.
At the end of the day, sidewall conveyor belts are engineered for specific jobs, so their materials are chosen to match that job. A belt for a small farm moving grain is totally different from a belt for a mine moving 100 tons of ore per hour, which is different from a belt for a food plant moving flour. There’s no “best” material overall—only the best mix for your exact needs.
If you’re in the market for a sidewall conveyor belt, or if you’ve had bad experiences with belts that don’t hold up, I’d love to chat. We work with all kinds of industries, from small farms to big mines, and we help you pick the exact material mix that fits your job, no guesswork. We don’t do cut-rate corners, we build belts that last. If you’re ready to talk specs, pricing, or just have more questions, feel free to reach out. I’m always happy to help.
Aramid Conveyor Belt References
- The Conveyor Equipment Manufacturers Association (CEMA) Standards for Conveyor Belt Design and Materials, 7th Edition, 2020.
- Rubber Chemistry and Technology, Vol. 92, No. 3, "Advances in Rubber Blends for Bulk Material Handling Conveyor Belts", 2019.
- Mine Safety and Health Administration (MSHA) Guidelines for Anti-Static Conveyor Belt Materials for Underground Mining Operations, 2021.
- Food and Drug Administration (FDA) Food Contact Substance (FCS) Notifications for Conveyor Belt Rubber Compounds, 2022.
- International Society of Automation (ISA) Standard for Conveyor System Material Compatibility Testing, 2020.
Alumina Technology (Qingdao) New Materials Co., Ltd.
As one of the most professional sidewall conveyor belt manufacturers and suppliers in China, we also support customized service. With abundant experience, we warmly welcome you to buy sidewall conveyor belt for sale here and get quotation from our factory. For price consultation, contact us.
Address: No.448, Jiangshan South Road, Huangdao District, Qingdao City, Shandong Province
E-mail: Gloria.zhang@contitech.cn
WebSite: https://www.altechconveyorbelt.com/
