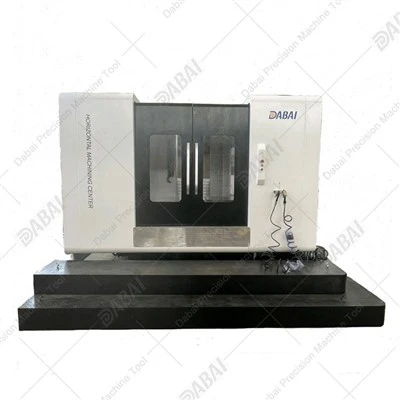
If you’ve ever walked through a precision manufacturing floor, you’ve probably seen a Horizontal Machining Center (HMC) humming away, its spindle rotating on a horizontal axis while a worktable spins parts through multiple sides without needing to reposition. As someone who’s spent the last 12 years supplying HMCs to job shops, aerospace facilities, automotive component makers, and even medical device manufacturers, I can tell you this machine isn’t a one-trick pony. A lot of new buyers assume HMCs only process a handful of common metals, but over the years, we’ve helped our clients cut, mill, and shape dozens of material types—some everyday, some specialized for harsh conditions, and even some that you might not expect to work well on a horizontal machining platform. Today, I want to break down exactly what materials our HMCs can process, why the platform is uniquely suited for each, and how to make the most of your HMC investment no matter what parts you’re running. Horizontal Machining Center
Let’s start with the workhorse of the manufacturing world: steel. This is what most of our new clients ask about first, and for good reason. Carbon steel, alloy steel, tool steel, and even stainless steel are all staples for HMCs, and the horizontal design makes these materials easier to machine than vertical mills for large, heavy parts. For example, a client of ours in the Midwest makes transmission gears for heavy-duty trucks from 4140 alloy steel—this material is tough, has high tensile strength, and requires consistent, deep cuts to get the gear teeth and bearing surfaces right. With an HMC, the worktable can hold the 500-pound part steady during long machining runs, and the horizontal spindle keeps chips falling away from the cut zone instead of nesting in the part or tool path, which reduces tool wear and cuts down on manual cleanup. We also supply HMCs to a medical equipment maker that machines 316L stainless steel for surgical instrument housings. The horizontal platform’s accuracy (most of our mid-range HMCs hold ±0.001 inch repeatability) means they hit the tight tolerances needed for sealing joints, and the high-pressure coolant system on our machines flushes fine metal shavings away, so no tiny particles get trapped in the crevices of the instrument. The key point here: steel is where HMCs shine, but it’s important to size the spindle horsepower correctly for your grade—high-alloy tool steel needs more torque than mild carbon steel, and we help clients match spindle specs to their steel material before purchase to avoid wasting tools or downtime.
Next up: aluminum, another super common HMC material, especially for aerospace and automotive lightweighting projects. I see a lot of people make the mistake of thinking aluminum is too soft to need an HMC, but that’s backwards. Aluminum’s low density means you can machine large, thin parts (like aircraft wing ribs or electric motor housings) that would wobble or warp on a vertical mill when repositioned. An HMC’s ability to access all four sides of a part in a single setup eliminates the need for multiple clampings, which not only saves time but also reduces the risk of part distortion from re-fixturing. One of our long-term clients in Texas produces heat sinks for EV batteries from 6061 aluminum—this alloy has excellent thermal conductivity, but it’s also prone to “chatter” when machined at high speeds. Our HMCs have dynamically balanced spindles that run up to 15,000 RPM, and the horizontal chip flow (aluminum shavings are long and stringy) means they don’t wrap around the tool or part mid-cut. We also recommend using our high-volume mist coolant system for aluminum, which cools the cut without leaving excess fluid that could mess with surface finishes, a critical factor for heat sinks. Even aluminum-lithium alloys, used in next-gen aircraft, work well on HMCs—their high strength-to-weight ratio makes them popular, and the horizontal platform’s rigid worktable can handle the vibration-free cuts needed to keep the alloy from galling.
Now, moving to materials that are a bit more specialized: non-ferrous metals beyond aluminum and copper. Copper and brass are used for electrical components, plumbing parts, and even decorative metalwork, and HMCs process these materials with great precision. Copper, especially electrolytic copper used for electrical connectors, is soft and ductile, so it can smudge if machined with a dull tool. Our HMCs’ automatic tool changers (ATCs) let clients switch to a sharp carbide or diamond-coated tool mid-cycle, so you don’t have to stop and re-tool manually, which keeps copper parts’ surface finishes smooth and free of burrs. A client in California that makes bus bars for solar inverters uses our 4-axis HMCs to mill and drill copper parts; the horizontal table’s indexing accuracy lets them mill 90-degree bends and mounting holes without human intervention, cutting their production time by 60% compared to their old vertical machines. Brass, too, is a go-to for HMCs—its machinability rating is higher than many steels, so it can be cut quickly, and the horizontal chip flow prevents brass shavings from sticking to the part, which is perfect for small, intricate components like valve stems or fittings.
What many people don’t realize is that HMCs aren’t just for metals—they process a wide range of plastics and composite materials, too. Engineering plastics like acetal (Delrin), nylon, and PEEK are used in everything from consumer electronics to automotive interior parts, and their low melting point means they can be prone to tool wear if not machined correctly. Our HMCs have variable spindle speed controls and the option for anti-vibration tool holders, which reduce heat buildup during cuts, preventing plastic parts from melting or deforming. A client we work with in the Pacific Northwest produces medical device components from PEEK, a high-performance biocompatible plastic used for orthopedic implants. The horizontal platform’s ability to process the entire part in one setup ensures that the implant’s surface is uniform, which is critical for biocompatibility, and the ATC can swap between a roughing and finishing tool without leaving tool marks that would require manual polishing. Even carbon fiber-reinforced polymer (CFRP), a super light composite used in aerospace and sports equipment, works on HMCs—CFRP’s abrasive fibers can wear tools fast, so we recommend diamond-coated tools for these runs, and our HMCs’ rigid structure prevents delamination during cutting. The horizontal table keeps the flat CFRP panel stable, so cuts are straight, and the chip evacuation system sucks up fine carbon fiber dust, which is both a safety hazard and can damage machine components if not removed.
Then there are the tough, heat-resistant materials that people used to think only could be machined on specialized vertical or 5-axis machines. High-temperature alloys (HTAs) like Inconel, Hastelloy, and titanium are used in jet engines, industrial furnaces, and oil and gas equipment, where parts have to withstand extreme heat and corrosion. These materials are notoriously difficult to machine—they have high strength at high temperatures, which means they generate a lot of heat during cuts, and they tend to work-harden, so a dull tool will tear the material instead of cutting it. HMCs are actually ideal for HTA processing because of their high-torque spindles (our heavy-duty HMCs have 50 HP spindles, compared to 20 HP for many entry-level vertical mills) and through-spindle coolant systems that deliver coolant directly to the cutting edge at pressures up to 1,000 PSI. One of our clients in Florida makes turbine blades for gas turbines from Inconel 718, a common HTA. The horizontal design lets them mount the blade vertically, so chips fall away instead of embedding in the blade’s cooling channels, which is a huge plus because embedded chips would ruin the part’s performance. We work with this client to set up custom tool paths and tooling for Inconel, and their cycle times are 30% faster than when they used a vertical mill for the same parts. Titanium, another tough alloy, is used for aerospace fasteners and medical implants, and HMCs handle it well too—its low thermal conductivity means heat builds up at the cutting edge, so the through-spindle coolant on our HMCs keeps the tool cool, extending tool life by up to 25% compared to other machine types for titanium runs.
I should also mention the materials that are better left for specialized equipment, just to set realistic expectations. HMCs aren’t the best choice for extremely soft, gummy materials like pure rubber, because the fast-spinning horizontal spindle can cause the material to wrap around the tool. They’re also not ideal for very thin, fragile materials like sheet metal foil, unless you have a custom fixturing setup. But for 90% of the high-precision, high-volume parts manufacturers make today, HMCs are versatile enough to handle the materials I’ve listed above.
Over the years, we’ve seen clients try to save money by buying the cheapest HMC on the market that doesn’t match their material needs, and it always comes back to bite them—downtime from tool wear, poor part tolerances, and extra manual work add up way more than investing in an HMC built for the materials you run. That’s why when a client reaches out, we first ask what materials they’ll be machining, part sizes, required tolerances, and production volume, then tailor a solution to fit their exact needs. Whether you’re running small, high-tolerance medical parts from PEEK or large steel transmission gears for heavy trucks, there’s an HMC configuration that works for you.
Vertical Machining Center If you’re evaluating new machining equipment and want to learn more about how an HMC can process your specific materials, or if you have questions about spindle specs, fixturing, or tooling for your material type, our team is here to help. We work with manufacturers of all sizes, from small job shops with 5 employees to large aerospace facilities with 500+ staff, and we can walk you through material-machine compatibility, case studies from similar clients, and even on-site demos to show our HMCs in action. Don’t guess at what your HMC can process—talk to the team that specializes in HMC solutions, and get tailored advice for your materials and production goals.
References
- Modern Machine Shop. (2022). Horizontal Machining Centers for High-Volume Precision Parts. Gardner Business Media.
- AST Materials. (2021). Machinability of Common Engineering Materials for CNC Equipment. American Society for Testing and Materials.
- Aerospace Manufacturing and Design. (2020). Processing High-Temperature Alloys with Horizontal Machining Platforms. Endeavor Business Media.
- SME. (2019). Non-Ferrous Metal Machining Best Practices for Horizontal Machining Centers. Society of Manufacturing Engineers.
- Composites World. (2022). Machining CFRP on Horizontal Machining Centers: Challenges and Solutions. Gardner Business Media.
Dabai Precision Machine Tool (Jiangsu) Co., Ltd.
As one of the most professional horizontal machining center manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to buy advanced horizontal machining center for sale here from our factory. We also accept customized orders.
Address: No. 66-1, Zhenhu North Road, Hudai Town, Binhu District, Wuxi City
E-mail: elaine@dabaicnc.com
WebSite: https://www.cnc-dabai.com/
